Introduction
A standard handheld infrared thermometer is well suited for quickly checking surface temperatures. However, in equipment verification, production quality control, laboratory testing, or temperature trend analysis, viewing a single reading is often not sufficient. Measurement results may also need to be stored, compared over time, or transferred to a computer for documentation.
An infrared thermometer with USB data export or PC communication extends non-contact temperature measurement beyond simple on-screen readings. It enables users to record, organize, analyze, and retain temperature data for later use.
USB functionality, however, is not essential for every application. Before selecting a model, it is important to determine whether the task requires only immediate temperature checks or also requires data storage, analysis, and traceability.
Key Points
● The main purpose of USB data functionality is not to improve measurement accuracy, but to support data storage, organization, analysis, and traceability;
● Industrial maintenance, product testing, quality inspection, laboratory research, and temperature trend monitoring are typical applications for infrared thermometers with USB communication;
● USB functionality varies by model and may include real-time PC communication, internal data export, or both;
● Temperature range, D:S ratio, emissivity, accuracy, response time, and data logging capability remain important selection criteria;
● For occasional spot checks where data retention is unnecessary, a standard infrared thermometer may be sufficient.
What Problem Does USB Data Export Solve?
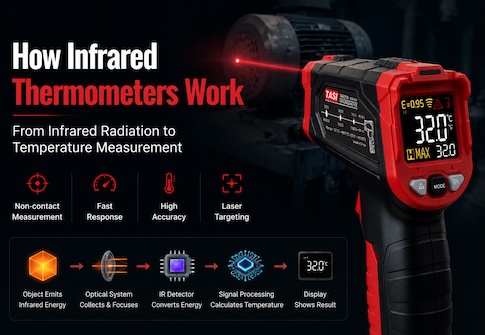
The primary function of an infrared thermometer remains the same: detecting infrared radiation emitted by a target surface and converting it into a temperature reading. A USB interface does not inherently improve measurement accuracy. Its main value lies in how measurement data can be managed.
When large numbers of readings need to be recorded, manual transcription is inefficient and can introduce errors. Depending on the instrument and its software, USB connectivity can allow measurement data to be transferred to a computer for storage, review, or further processing.
Typical uses include:
● Storing multiple temperature readings for measurement records;
● Viewing temperature changes over time;
● Comparing readings from different equipment, locations, or production batches;
● Exporting data for inspection or quality reports;
● Retaining original measurement data for maintenance, testing, and fault analysis.
USB communication therefore becomes especially useful when temperature results form part of a quality-control, laboratory, or maintenance process.
Which Industrial Maintenance Applications Benefit Most?
In industrial maintenance, identifying a single hot spot can be useful, but many developing faults are better assessed by comparing measurements over time.
Motors, bearings, gearboxes, pumps, electrical equipment, and mechanical transmission components may show gradually increasing surface temperatures during operation. If temperatures are recorded during each inspection, maintenance personnel can compare readings from different dates and identify abnormal trends.
Typical applications include:
● Equipment temperature-rise testing;
● Preventive maintenance records;
● Temperature comparison of motors, bearings, and mechanical components;
● Detection of abnormal heating in electrical equipment;
● Before-and-after maintenance temperature comparison.
Infrared thermometers measure surface temperature. Measurement distance, target area, surface material, and emissivity can all affect readings. For meaningful long-term comparisons, measurement position and conditions should therefore be kept as consistent as possible.
Why Is Data Export Useful in Production Quality Inspection?
In manufacturing, temperature measurements are often used not simply to obtain a single value, but to confirm that products or processes remain within an acceptable temperature range.
Applications in plastics processing, electronics assembly, mechanical manufacturing, surface treatment, and heating or cooling processes may require temperature data from different products, batches, or workstations to be documented.
An infrared thermometer with USB data capability can reduce manual recording and make batch comparison and quality traceability more efficient.
Typical uses include:
● Final-product temperature inspection;
● Verification of heating and cooling processes;
● Temperature comparison between production batches;
● Before-and-after comparison following process adjustments;
● Quality investigation and data archiving.
Where temperature results form part of an internal quality record, data communication capability can be more useful than functions that only display instantaneous MAX or MIN values.
Why Do Laboratories and R&D Applications Benefit from USB Communication?
Laboratory and development work generally places greater emphasis on complete and reproducible data.
During material testing, electronic product evaluation, mechanical verification, or thermal performance studies, engineers may need to monitor how a surface temperature changes over tens of seconds, several minutes, or longer periods. Manually reading the display makes it difficult to capture the full temperature profile.
An infrared thermometer with PC communication can provide more complete measurement records and simplify subsequent trend analysis and comparison between test conditions.
Typical applications include:
● Temperature-rise testing of electronic components and PCBs;
● Thermal performance evaluation;
● Material heating and cooling experiments;
● Operating-temperature verification of mechanical components;
● Comparison of different design configurations.
For these applications, users should consider not only USB connectivity but also logging interval, storage capacity, time-stamp capability, and software functions.
What Are the Advantages in Electrical and Electronic Testing?
Power supplies, printed circuit boards, connectors, transformers, battery assemblies, and other electrical or electronic devices may generate heat during operation. Engineers often need to determine whether temperatures stabilize and how they change under different loads.
Infrared measurement provides a non-contact method for quickly checking multiple locations without attaching a probe directly to the surface.
USB communication adds further value by allowing measurements from different points or test stages to be stored and compared for:
● No-load versus loaded temperature comparison;
● Temperature-rise testing at different power levels;
● Thermal design optimization;
● Product reliability testing;
● Prototype versus production-unit comparison.
When measuring small electronic components, the D:S ratio is especially important. The measurement spot must remain appropriately sized relative to the target; otherwise, radiation from surrounding surfaces may influence the reading.
Why Is USB More Useful When Monitoring Temperature Trends?
Many measurement tasks focus less on one absolute temperature value and more on how temperature changes over time.
Equipment may gradually heat after startup and cool after shutdown. Manufacturing processes may also require monitoring how a product temperature changes through heating, processing, and cooling stages.
When measurement data can be transferred to a computer via USB, it becomes easier to evaluate:
● Heating rate;
● Cooling behavior;
● Time at which peak temperature occurs;
● Whether temperature reaches a stable condition;
● Differences between test conditions.
For trend analysis, the sampling or logging rate must also be suitable for the process. If the target temperature changes rapidly but the recording interval is too long, important transitions may not be captured.
Are USB Data Export and Real-Time PC Communication the Same Thing?
Not necessarily.
Manufacturers may use the term “USB function” for different capabilities. Some instruments allow internally stored measurements to be downloaded to a computer, while others can transmit readings continuously during measurement. Some models support both functions.
Before purchasing, confirm:
● Whether real-time PC communication is supported;
● Whether the instrument includes internal data memory;
● How many readings can be stored;
● Whether the logging interval can be configured;
● Whether the software supports graphical trend display;
● Whether data can be exported in commonly used file formats;
● Whether the software is compatible with the required computer operating system.
If measurements only need to be collected in the field and reviewed later, internal memory with USB export may be sufficient. If continuous process observation is required, real-time communication is more important.
What Other Specifications Should Be Considered?
USB is an auxiliary feature. Whether an instrument is suitable for the measurement task still depends primarily on its infrared measurement performance.
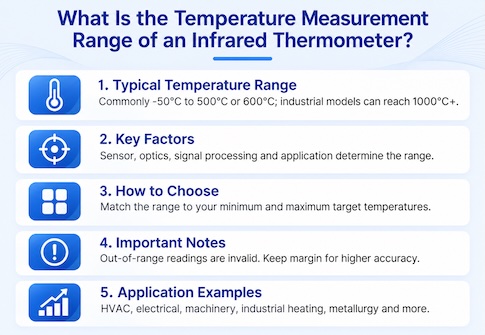
● Temperature range: The measurement range should cover the actual target temperatures with reasonable margin. A wider range does not automatically provide better accuracy in every application.
● D:S ratio: D:S determines the measurement spot size at a given distance. Long-distance measurement of small targets generally requires a higher D:S ratio, and the target should be larger than the effective measurement area.
● Emissivity setting: Metals, plastics, coatings, rubber, and other materials have different emissivity characteristics. Adjustable emissivity is preferable when multiple surface types must be measured.
● Accuracy and repeatability: Quality inspection and laboratory testing require not only suitable specified accuracy but also consistent readings under repeatable conditions.
● Response time: Moving targets and rapidly changing surfaces require sufficiently fast response to follow the actual temperature change.
● Data logging capability: Check memory capacity, logging interval, time information, and PC software functions.
● Operating environment: High temperatures, dust, oil mist, steam, and large ambient-temperature changes can influence practical measurement performance.
When Is USB Functionality Unnecessary?
More functions do not always mean a better instrument for a particular application.
If the primary task is simply to perform occasional spot checks—for example, identifying overheating in HVAC components, machinery, heating systems, or routine maintenance—and there is no need to retain large quantities of data, a standard infrared thermometer may be sufficient.
USB functionality is generally less important when:
● Only occasional single-point measurements are required;
● The purpose is simply to identify whether a temperature is abnormal;
● Historical temperature records are not required;
● Measurement data does not need to be transferred to a computer;
● Temperature curves or formal reports are unnecessary.
In these cases, it may be more useful to prioritize temperature range, D:S ratio, accuracy, or adjustable emissivity rather than adding unnecessary communication functions.
How Can You Decide Whether You Need a USB Infrared Thermometer?
A practical question is: what happens to the measurement data after the temperature has been read?
If the reading is only needed at the time of inspection, USB functionality may offer little additional value.
If the data must later be used for reports, comparison, trend analysis, quality traceability, experimental verification, or maintenance records, USB communication becomes much more useful.
Consider the following:
● Do dozens, hundreds, or more temperature readings need to be stored?
● Do temperature changes need to be compared across different dates?
● Must test records be submitted to customers, engineering teams, or quality departments?
● Is computer-based temperature trend analysis required?
● Is reducing manual data transcription important?
If several of these requirements apply, an infrared thermometer with USB data communication is generally a more appropriate choice.
FAQ
● Does a USB infrared thermometer provide better measurement accuracy?
Not necessarily. USB is mainly used for communication and data management. Measurement accuracy still depends on the infrared sensor, optics, calibration, emissivity settings, and measurement conditions.
● Can a USB infrared thermometer remain connected to a computer during measurement?
It depends on the model. Some instruments support real-time PC communication, while others only allow internally stored data to be downloaded.
● Can USB-exported data be used directly in quality reports?
It can serve as a measurement-data source, but suitability for a formal quality system depends on the software records, testing procedure, and the organization’s own documentation requirements.
● Is USB required for creating a temperature curve?
USB communication is useful when a large number of readings need to be transferred to a computer for trend analysis. However, the instrument must support continuous communication or automatic logging.
● For long-distance measurement, which is more important: USB or D:S?
D:S is more important for the measurement itself. USB manages data, while D:S determines the size of the target area measured at a given distance.
● Can the USB port power the infrared thermometer?
Not necessarily. Some USB ports are used only for communication. Power functionality should always be confirmed in the instrument specifications.
Summary
Infrared thermometers with USB data export are most useful when an application requires not only temperature measurement, but also the storage, analysis, comparison, and traceability of temperature data.
Industrial maintenance, production quality inspection, laboratory R&D, electrical and electronic testing, product validation, and temperature trend analysis are typical applications. PC communication can reduce manual transcription and provide a more complete basis for data comparison, fault analysis, and test reporting.
USB connectivity should not, however, be the only selection criterion. Temperature range, D:S ratio, emissivity setting, measurement accuracy, response time, and logging method remain fundamental to determining whether an infrared thermometer is suitable for the task.
For simple spot checks, a standard infrared thermometer is often sufficient. For applications requiring systematic recording, analysis, and traceability, a model with USB data communication offers clear practical advantages.